
Four Process Factors and Improvement Measures that Affect the Surface Roughness of Precision Parts Processing
author: Hansheng Automation
2023-05-18
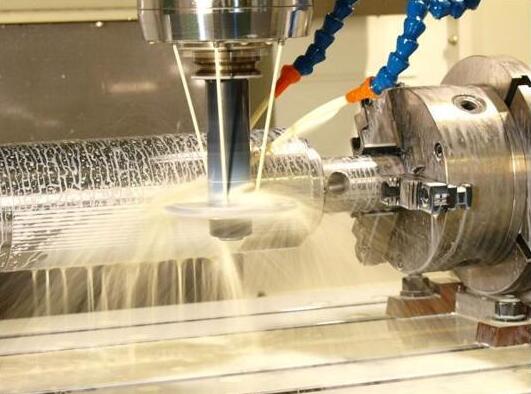
In the machining process of precision parts, the residual area caused by the geometric shape and cutting motion of the tool, the grooves scratched by the tool's chip accumulation, the vibration ripple caused by the vibration between the workpiece and the tool, and the extrusion and friction marks caused by the tool's side wear can cause the surface roughness of the parts. The process factors that affect surface roughness mainly include workpiece material, cutting amount, tool geometric parameters, and cutting fluid.
1. Workpiece material: Generally speaking, elastic-plastic materials with higher toughness have higher surface roughness values after processing, while elastic-plastic materials with lower toughness are more likely to obtain smaller surface roughness values after processing. For the same material, the larger the grain structure, the greater the roughness value of the machined surface. Therefore, in order to reduce the surface roughness value of machining, the material is often quenched and tempered or normalized before machining the cutting surface to obtain uniform and fine grain structure and larger hardness.
2. Cutting amount: The higher the feed speed, the higher the height of the residual area, and the rougher the surface of the part. Therefore, reducing the feed rate can effectively reduce the surface roughness value. Cutting speed also has a significant impact on surface roughness. When cutting elastic-plastic materials at medium speed in precision parts processing, it is easy to generate chip buildup and large plastic deformation, resulting in a higher surface roughness value of the workpiece being processed. Usually, low-speed or high-speed cutting of elastic-plastic materials can effectively avoid the formation of chip deposits and have a positive effect on reducing surface roughness values.
3. The geometric parameters of the tool: the main deviation angle, secondary deviation angle, and tool tip radius have a direct impact on the surface roughness of the part. When the feed rate is constant, reducing the main and auxiliary deviation angles or the radius of the large tool tip arc can reduce the surface roughness value. In addition, increasing the front and back angles appropriately can reduce cutting deformation and surface friction, suppress the generation of chip deposits, and also reduce surface roughness values.
4. Cutting fluid: The cooling and lubricating effects of cutting fluid can reduce friction during the cutting process, lower the temperature of the cutting zone, reduce the plastic deformation of the metal surface of the cutting layer, and suppress the generation of chip deposits during precision parts processing, thus greatly reducing the surface roughness value.
The Importance of CNC Precision Machining in the CNC Processing Industry
Two minute understanding, three methods for determining machining allowance in precision parts processing
Related Article

Let us go over the foundations of the electroplating procedure. Electroplating involves several phases, and from pre-treatment to post-treatment there are several really significant ones.
The basic principle of surface treatment of precision parts in CNC machining

Audio panels, electronic cigarette shells, nameplateLOG, watch shells, etc. are among the CNC processing of high surface texture needs components.
CNC machining aluminum alloy parts high-quality surface texture process explained in detail

Metallic finishing, sometimes known as metallic finishing, is the process of using several techniques to change the surface of an object in order to improve appearance and performance, such as corrosion resistance, discoloration resistance, chemical resistance, abrasion resistance, and hardness, modify electrical conductivity, remove burrs, or apply a specific color to a machined part.
Metal CNC finishing surface treatment process and its working principle
