
Requirements for superhard abrasive machining of precision parts
author: Hansheng Automation
2023-05-15
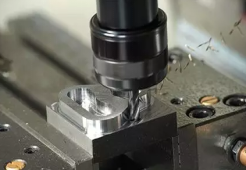
The grinding of superhard abrasive micro powder grinding wheels can be carried out on CNC precision parts processing grinders. Precision grinding should be carried out on the corresponding CNC precision parts processing grinder. However, due to the small size of micro powder particles, the grinding machine should have micron level grinding. The feed system ensures the required grinding depth. In fact, superhard grinding wheels have some requirements for grinding machines, and it is best to perform grinding processing on superhard grinding wheels. The requirements for grinding machines with superhard grinding wheels mainly include the following aspects.
1. Grinder accuracy should be high. In the rotation accuracy of the grinding wheel spindle, the radial circular runout should be<0.001 mm, and the axial circular runout should be<0.005 mm. The main shaft bearings are mostly dynamic pressure bearings or combination bearings, and static pressure bearings can also be used. To ensure the machining accuracy required for precision grinding.
2. The grinding machine must have sufficient rigidity, high stability, and low vibration. The stiffness of machine tools can affect the stability and vibration resistance of the grinding process, thereby affecting the durability and lifespan of superhard abrasive wheels, and also affecting the quality of the grinding process. The general requirement is to increase the stiffness by about 50% compared to ordinary grinding machines.
3. Ultra hard abrasive wheels have low vibration during grinding. The machine tool should be placed on an anti vibration foundation and corresponding anti vibration and isolation measures should be taken. For example, grinding wheels need to be finely trimmed and balanced, and anti vibration pads should be added at the contact between the machine tool and the ground.
4. A good feed system is required, with high accuracy, uniform and stable speed, wide speed range, high speed to ensure productivity requirements, and low speed to ensure grinding size, shape accuracy, and surface roughness requirements. The minimum longitudinal feed rate should generally be 0. lm/min or even smaller, and the minimum transverse feed rate (grinding depth) should be 0.001-0.0005 mm/8t (st ^ single stroke). For micro powder grinding, the matching between the feed speed of the grinding machine and the size of the abrasive particles should be considered.
The Impact of Precision Parts Processing Technology on Industry
What are the main requirements for the use environment of precision machining centers
Related Article

Let us go over the foundations of the electroplating procedure. Electroplating involves several phases, and from pre-treatment to post-treatment there are several really significant ones.
The basic principle of surface treatment of precision parts in CNC machining

Audio panels, electronic cigarette shells, nameplateLOG, watch shells, etc. are among the CNC processing of high surface texture needs components.
CNC machining aluminum alloy parts high-quality surface texture process explained in detail

Metallic finishing, sometimes known as metallic finishing, is the process of using several techniques to change the surface of an object in order to improve appearance and performance, such as corrosion resistance, discoloration resistance, chemical resistance, abrasion resistance, and hardness, modify electrical conductivity, remove burrs, or apply a specific color to a machined part.
Metal CNC finishing surface treatment process and its working principle
