
What should be paid attention to when milling curved surfaces on large CNC machining centers
author: Hansheng Automation
2022-08-30
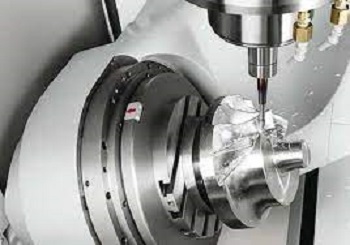
Large CNC machining centers are high-efficiency automated machine tools composed of mechanical equipment and CNC systems suitable for processing complex parts. CNC machining centers are one of the highest production and most widely used CNC machine tools in the world.
1. In milling curved parts, if it is found that the material of the part has poor heat treatment, cracks, uneven organization, and other phenomena, the processing should be stopped in a timely manner to avoid wasting time.
2. When milling complex surfaces in the mold cavity, a longer cycle is usually required. Therefore, before starting the milling process, the machine tool, fixture, and tool should be properly inspected to avoid malfunctions that may affect the machining accuracy or even cause waste.
3. Precision machining ultimately produces a theoretical surface. When precision machining curved surfaces with ball end milling cutters, the line cutting method is generally used. For parts with good openness, the turning point for line cutting should be selected outside the curve table, that is, during programming, the surface should be extended outwards.
4. When milling a curved surface with a ball end milling cutter, the cutting speed at the tip is very low. If a ball end milling cutter is used to mill a relatively flat curved surface perpendicular to the machined surface, the surface quality cut by the ball end milling cutter tip is relatively poor. Therefore, the spindle speed should be appropriately increased, and cutting with the tip should also be avoided.
5. Avoid vertical cutting. There are two types of flat bottomed cylindrical milling cutters. One is that the end face has a pointed hole, and the end edge is not at the center. Another method is to have no tip hole on the end face, with the end blades connected and passing through the center. When milling curved surfaces, an end milling cutter with a pointed hole must not feed vertically downwards like a drill bit, unless a process hole is pre drilled.
If the CNC machining center uses an end tool without a center hole, it is possible to feed vertically downwards, but due to the small blade angle and high axial force, it should also be avoided as much as possible. The best method is to feed diagonally downwards, and then cut laterally with the side blade after reaching a certain depth.
What are the methods for obtaining dimensional accuracy during precision part machining
Analysis on the Determination of Process Dimensions and Their Tolerances in Five Axis Machining of Parts in a Five Axis Machining Center Factory
Related Article

Let us go over the foundations of the electroplating procedure. Electroplating involves several phases, and from pre-treatment to post-treatment there are several really significant ones.
The basic principle of surface treatment of precision parts in CNC machining

Audio panels, electronic cigarette shells, nameplateLOG, watch shells, etc. are among the CNC processing of high surface texture needs components.
CNC machining aluminum alloy parts high-quality surface texture process explained in detail

Metallic finishing, sometimes known as metallic finishing, is the process of using several techniques to change the surface of an object in order to improve appearance and performance, such as corrosion resistance, discoloration resistance, chemical resistance, abrasion resistance, and hardness, modify electrical conductivity, remove burrs, or apply a specific color to a machined part.
Metal CNC finishing surface treatment process and its working principle
