
Five Axis Machining Center Factory Tells How to Clean Winding Chip in Stainless Steel Five Axis Machining
author: Hansheng Automation
2022-03-15
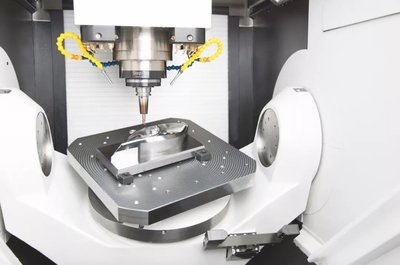
The 5-axis machining center factory generally controls the simultaneous movement of three linear coordinate axes and two rotating coordinate axes for stainless steel 5-axis machining CNC machine tools, enabling the cutting tools and workpieces to cut and process according to the specified motion trajectory. It is suitable for machining complex surface parts such as blades, propellers, and wings.
Due to the vertical machining direction of the spindle and tool in the five axis machining center, the cutting chips generated by the stainless steel five axis machining center during operation often adhere to the tool.
Especially when machining holes, the tool must be wrapped with long chips. Failure to clean these chips in a timely manner may entangle them in the tool changing arm, causing damage to the cutting edge. If wrapped in the tool probe, it can cause the tool probe to malfunction. If the chips wrapped on the tool of the five axis machining center are not cleaned in a timely manner, it can scratch the surface of the workpiece, and in severe cases, it can damage the original components of the five axis machining center, affecting the service life of the equipment.
So, can the chips wrapped around the stainless steel five axis machining center tool be manually cleaned?
In general, long strip shaped chips are sharper and tightly wound. To solve the problem of winding chips, it is necessary to start from the beginning by setting the feed rate.
Firstly, during processing, it is possible to increase the feed speed appropriately and attempt to automatically break these chips. Using the correct fixed cycle, try to break and get rid of these chips. Adjust the coolant nozzle in place to wash away these chips.
Secondly, using the correct five axis machining programming and processing procedures can also effectively limit winding cutting problems. For example, using a right rotating tool for forward milling, machining a simple part and drilling, will produce a series of slender cutting chips that will wrap around the tool until they form a large ball. If the spindle is rotated in reverse between the processed holes, it can shake off these chips before they have a chance to wrap together.
Finally, it is important to ensure that the safety plane is far enough from the workpiece to provide appropriate separation space for the chips. Using manual programming, it is necessary to increase the spindle rotation during the dwell time after each hole processing.
Under normal circumstances, the spindle rotation is sufficient to cause the chips to detach from the tool.
How to solve the problem of the spindle not rotating in large CNC machining centers
What factors are related to precision in analyzing precision parts processing
Related Article

Let us go over the foundations of the electroplating procedure. Electroplating involves several phases, and from pre-treatment to post-treatment there are several really significant ones.
The basic principle of surface treatment of precision parts in CNC machining

Audio panels, electronic cigarette shells, nameplateLOG, watch shells, etc. are among the CNC processing of high surface texture needs components.
CNC machining aluminum alloy parts high-quality surface texture process explained in detail

Metallic finishing, sometimes known as metallic finishing, is the process of using several techniques to change the surface of an object in order to improve appearance and performance, such as corrosion resistance, discoloration resistance, chemical resistance, abrasion resistance, and hardness, modify electrical conductivity, remove burrs, or apply a specific color to a machined part.
Metal CNC finishing surface treatment process and its working principle
